Powder discharge problems are common in chemical plants handling fine, cohesive, hygroscopic, or easily agglomerated powders. Poor flowability, moisture absorption, particle adhesion, wall buildup, and agglomeration can make powder difficult to discharge from silos and hoppers, resulting in unstable feeding, production interruptions, and increased maintenance requirements.
Similar discharge problems can also occur in cement plants, where bridging, ratholing, wall buildup, and poor powder flowability can reduce discharge efficiency. See our guide to silo discharge problems in cement plants.
1. What Are the Common Powder Discharge Problems?
Fine powders can be difficult to discharge from silos and hoppers because of poor flowability, particle cohesion, moisture sensitivity, and wall adhesion. These characteristics can cause several common powder discharge problems, including:
- Bridging – Powder forms a stable arch above the outlet, preventing material from discharging.
- Ratholing – Material flows mainly through a central channel while powder remains along the silo walls.
- Caking – Moisture, pressure, or prolonged storage causes powder to harden into compacted masses.
- Wall buildup – Fine powder adheres to the silo wall and gradually reduces the effective flow area.
- Intermittent discharge – Material flow starts and stops instead of remaining stable and continuous.
- Incomplete discharge – A significant amount of powder remains inside the silo after discharge.
- Unstable feeding – Irregular powder flow causes fluctuations in downstream feeding or batching.
2. What Causes Powder Discharge Problems?
2.1 Poor Powder Flowability
Poor powder flowability is one of the main causes of powder discharge problems in silos and hoppers. Fine chemical powders often have small particle sizes and high cohesion, which can increase internal friction and make the material less likely to flow under gravity. Poor flowability can contribute to bridging, ratholing, intermittent discharge, and incomplete emptying.
2.2 Moisture Absorption
Many fine powders are sensitive to moisture. When moisture enters a silo or hopper, particles can become more cohesive and adhesive, increasing the risk of caking and wall buildup. Humid storage conditions, inadequate silo sealing, and moisture entering through inspection openings or other connections can further worsen powder flowability.
2.3 Particle Agglomeration and Caking
Fine powders can agglomerate during storage, particularly when particles are cohesive or exposed to moisture and pressure. As agglomerates become larger and harder, they can restrict the outlet and contribute to bridging, unstable discharge, or incomplete material flow.
2.4 Silo Wall Buildup
Powder buildup on silo walls can progressively reduce the effective flow area and interfere with material movement toward the outlet. Adhesive powders may accumulate on the wall, particularly around the conical section, and repeated buildup can eventually contribute to bridging, ratholing, and recurring discharge problems.
2.5 Long Storage Time
Extended storage can increase the risk of powder compaction, agglomeration, and caking. When fine powders remain stationary for long periods, the material may become less flowable and more difficult to discharge, especially under humid conditions or when the powder has strong cohesive properties.
2.6 High Wall Friction
High friction between the powder and the silo wall can restrict downward material movement. Rough internal surfaces, accumulated material, or the natural properties of certain powders can increase wall friction and contribute to poor flow, ratholing, and incomplete discharge.
2.7 Unsuitable Silo or Hopper Geometry
Silo and hopper geometry also affects powder discharge performance. Factors such as silo diameter, outlet diameter, hopper or cone angle, wall surface condition, and outlet configuration can influence the flow pattern and determine whether material flows evenly toward the outlet.
3. Conventional Solutions for Powder Discharge Problems
Vibrators
Vibrators can improve material movement in some applications, but their performance varies with the powder and the silo conditions.They may be less effective when cohesive powder has formed a hard layer on the silo wall.
Air Cannons
Air cannons use a sudden release of compressed air to break certain types of blockage.Their effectiveness depends on the blockage location, material properties, silo geometry, and how compacted the blockage has become.
Manual Cleaning
Manual cleaning can remove heavy buildup, but it requires access to the equipment and may require the production line to be stopped.
These methods can be useful for specific operating conditions, but their effectiveness depends on powder properties, blockage location, silo geometry, and the severity of buildup or caking.
4. Mechanical Flow Assistance for Difficult-Flowing Powders
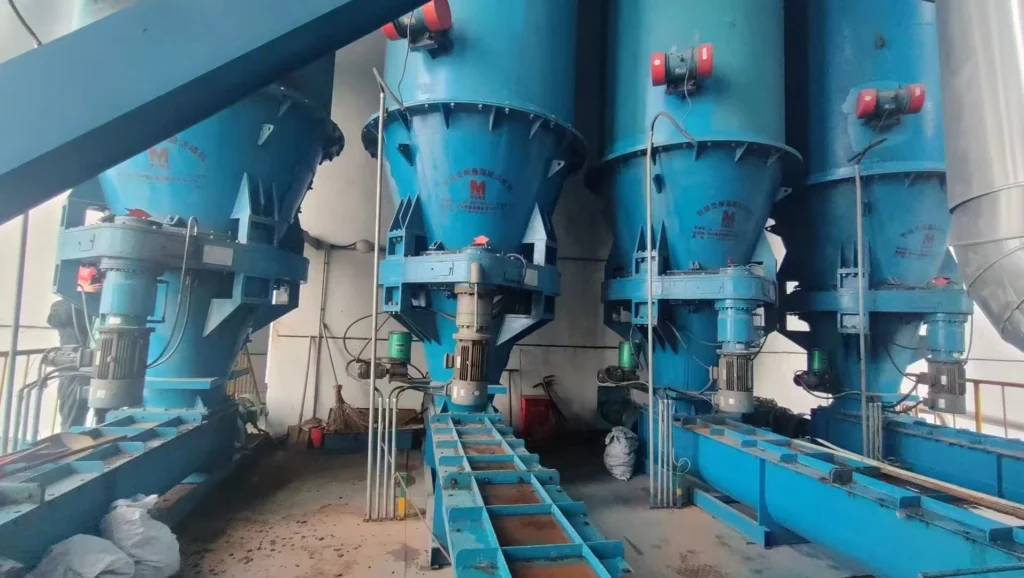
HNMY’s Intelligent Variable Inclination Vortex Anti-Blocking Machine can be applied to existing silos handling difficult-flowing powders, making it suitable for retrofit applications where replacing the existing silo is impractical. Its 360° rotating scraper works along the inner silo wall to continuously remove accumulated material and reduce the conditions that contribute to bridging, ratholing, and wall buildup.
The system can operate continuously online, helping maintain more stable material flow without requiring frequent manual cleaning or complete system shutdowns.
5.Powder Discharge Problems and Solutions
| Powder discharge problem | Typical symptom | Possible cause | Possible solution |
|---|---|---|---|
| Bridging | No material exits the outlet | Cohesion / arch formation | Mechanical flow assistance |
| Ratholing | Material flows mainly through the center | Poor flowability / wall friction | Flow-aid system |
| Caking | Hardened powder restricts discharge | Moisture / long storage | Moisture control + flow assistance |
| Wall buildup | Powder adheres to silo walls | Adhesion / moisture | Wall flow assistance |
| Intermittent discharge | Unstable feeding | Buildup / arching | Continuous flow assistance |
| Incomplete discharge | Residual powder remains in silo | Poor flow pattern | Flow optimization |
6. Powder Buildup and Cross-Contamination Risks
In fine chemical, electronic chemical, pigment, and other high-purity applications, residual material inside storage and handling equipment can create additional quality concerns.
Material accumulated on silo walls may detach during operation or product changeover and enter the next batch, potentially affecting product consistency or causing cross-contamination.
This makes regular control of wall buildup and stable discharge especially important in high-purity powder handling.
7. Dust Emissions and Static Electricity
Fine powders can generate dust during conveying, feeding, batching, and discharge.
Combustible or reactive powders may also require additional measures for dust control, grounding, and static-electricity management.
Dust emissions can affect workshop cleanliness, material recovery, and operating conditions. For chemical plants handling high-value powders, material loss caused by dust dispersion can also increase production costs over time.
For chemical plants facing recurring powder discharge problems, the appropriate solution depends on powder properties, moisture conditions, silo geometry, and the severity of buildup or blockage. For existing silos, a customized mechanical flow-assistance or anti-blocking solution can help improve discharge stability without replacing the entire storage system.